A pressure relief valve does nothing for years, right up until the one moment it absolutely has to work. That's exactly what makes PRV testing different from almost every other calibration or verification discipline: you're not checking whether an instrument reads accurately during normal operation, you're confirming a safety device will actually respond correctly during an overpressure event it may never experience until the day it matters most.
This is why PRV testing UAE refineries, petrochemical plants, and process facilities depend on follows some of the most rigorous documented standards in industrial testing. This guide covers how PRV testing actually works, the standards governing it, and what a complete certification process looks like.
Why Pressure Relief Valves Demand This Level of Scrutiny
PRVs are some of the most important pieces of equipment in a plant, protecting systems from overpressure events that can damage equipment and, in some cases, lead to catastrophic consequences. A relief valve sits in a unique operational category: it spends the vast majority of its service life doing nothing, seated closed under normal system pressure, and is only called upon during an abnormal event. This creates a specific verification challenge, since you can't simply observe the valve during routine operation to confirm it's working correctly. You need to actually test it against known conditions to confirm it will perform when genuinely needed.
Not every valve or application can be solved with a single testing solution. The required level of performance, the condition of the valve, and the actual service conditions it operates under all vary, which is why PRV testing programs need to be built around the specific valve and its application rather than a generic checklist.
The Two Core Tests: Pop Testing and Seat Tightness
A complete PRV certification process generally addresses two distinct performance characteristics, and understanding the difference matters for interpreting what a passed test actually confirms.
Pop Testing
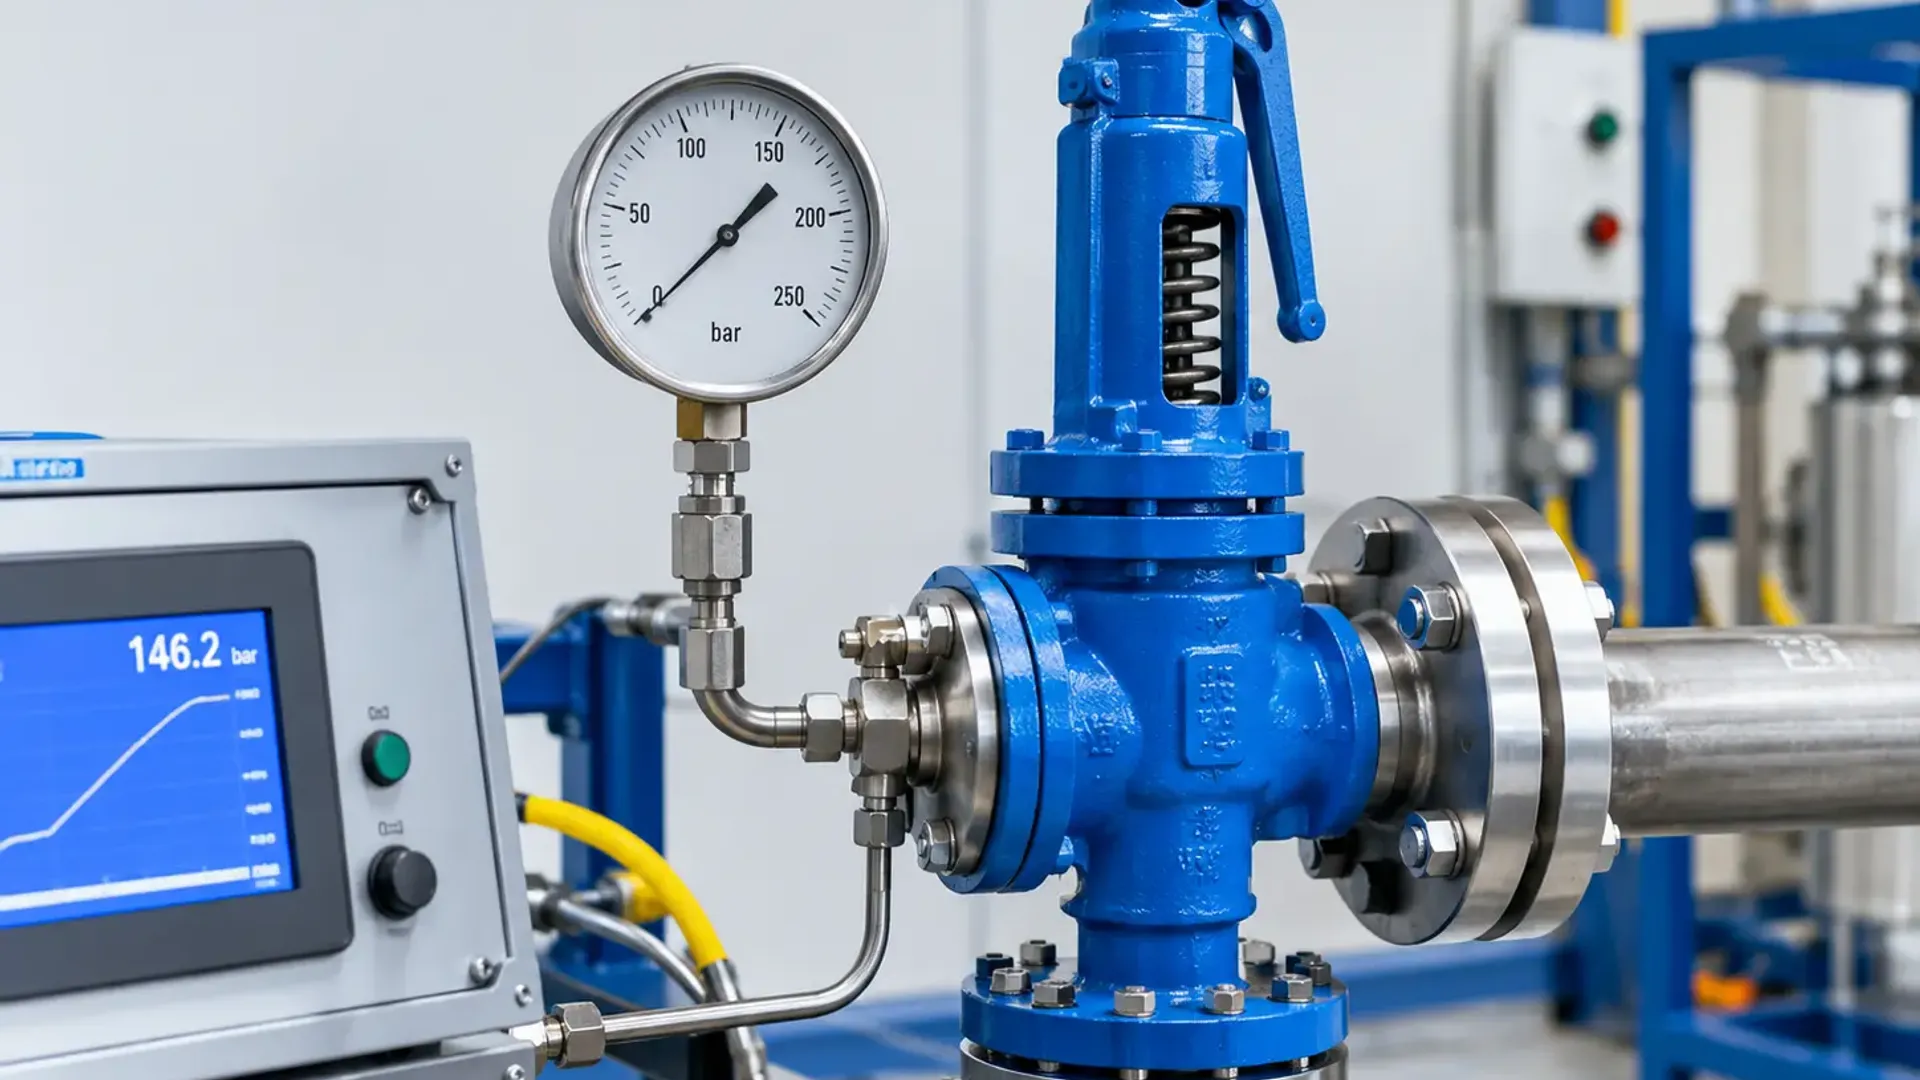
Pop testing verifies the pressure at which the valve actually opens, confirming it lifts at its stated set pressure within the tolerance allowed by the applicable code. This is tested by gradually increasing pressure at the valve inlet until the valve audibly and visibly "pops" open, with the actual opening pressure recorded and compared against the valve's nameplate set pressure.
Seat Tightness Testing
Seat tightness testing, governed primarily by API Standard 527, verifies the valve doesn't leak while in its closed position under normal operating pressure. This is tested by holding pressure at the valve inlet at a percentage of set pressure, commonly 90% for valves set above 50 psi, and measuring any leakage against defined acceptance criteria. Metal-seated valves are typically held to a stricter maximum allowable leakage rate than soft-seated valves, which are generally expected to show no leakage at all during the test period.
Standards Governing PRV Testing
PRV testing UAE facilities rely on typically references several complementary standards, each covering a different aspect of the testing and certification process:
API 576 governs the inspection, testing, repair, and documentation requirements for pressure relief valves, rupture discs, and safety relief valves specifically in petroleum refining and related industries, and is typically the primary standard driving overall inspection intervals and procedures.
API 527 specifically covers seat tightness testing methodology and the maximum acceptable leakage rates for both metal-seated and soft-seated pressure relief valves, including conventional, bellows, and pilot-operated designs. It specifies procedures using air or nitrogen, steam, or water, chosen based on the valve's actual service medium.
BS EN ISO 4126 is the international standard equivalent, using the generic term "safety valve" rather than the American Petroleum Institute's "pressure-relief valve" terminology, though both refer to functionally equivalent devices and testing principles.
API 598 covers valve inspection and testing more broadly, often referenced alongside API 527 and API 576 for comprehensive valve certification programs.
The Full Testing Process Step by Step
A properly executed PRV test generally follows this sequence:
- Initial visual inspection of the valve inlet and outlet for corrosion, clogging, signs of leakage, mechanical damage, or wear
- Verification of nameplate data against the process design pressure, confirming the valve's stated set pressure matches what the system actually requires
- Pop testing to confirm the valve lifts at its correct set pressure within code tolerance
- Seat tightness testing per API 527, using the appropriate test medium for the valve's actual service, air or nitrogen for compressible fluid service, water for non-compressible service
- Body testing, checking the valve's structural integrity under test conditions
- For bellows or closed bonnet valves, additional leak testing of the bellows and bonnet assembly itself
- Documentation of all results, including as-found and as-left condition, and affixing a tag or seal confirming the test date and result
If a valve fails pop testing or seat tightness testing, it typically requires adjustment, lapping of the seat surface to restore proper contact, spring replacement, or in some cases full valve replacement before it can be recertified and returned to service.
Common Failure Modes PRV Testing Catches
Testing regularly identifies specific, well-documented failure patterns:
- Seat leakage or chattering, often caused by the valve being oversized relative to its application, with the set pressure too close to normal operating pressure, leaving insufficient headroom
- Simmer, a subsonic leakage occurring before the valve fully lifts, typically caused by a worn or corroded seat that requires lapping to re-establish proper contact
- Spring degradation, identified by comparing measured free length and compressed length against the manufacturer's original specification
- Corrosion or mechanical damage at the inlet or outlet, potentially restricting flow during an actual relief event even if the valve itself would otherwise open correctly
What Determines Your Testing Frequency
The frequency of checking relief valves is one of the most common questions facilities ask, and the honest answer is that a definite testing interval should be established for every pressure relieving device individually, since not every valve or application can be solved with the same fixed schedule. Key factors influencing appropriate testing frequency include:
- The type of service medium the valve is exposed to, since corrosive or fouling services accelerate degradation
- The valve's operating history and any prior test results showing developing wear patterns
- Regulatory or insurance requirements specific to the facility's industry and jurisdiction
- Manufacturer-recommended intervals as a baseline, adjusted based on actual observed performance over time
Operating experience at a specific installation should inform and refine the testing interval over time, rather than applying a single generic schedule across every valve regardless of its actual service conditions.
Complete Documentation: What API 576 Requires
Comprehensive documentation is a core requirement of a proper PRV testing program, typically including the valve's tag number and service, its set pressure, the test date, as-found and as-left condition, and the test technician's signature. A complete record should also cover spring inspection details comparing measured values against manufacturer specification, the seat tightness test result including test pressure and measured leakage rate, any parts replaced during servicing with their manufacturer part numbers, nameplate data verification against the process design pressure, and a recommended next inspection date.
This level of documentation matters because PRV compliance is typically mandated by process safety management programs, insurance requirements, and regulatory bodies, all of which expect a defensible, complete record rather than a simple pass or fail stamp.
ISO 17025 Accredited PRV Testing Across the UAE
General Tech Services offers both on-site and in-house testing of PRVs, ranging from ¼ inch to 12 inches, under EIAC and ENAS ISO 17025 accreditation, covering testing to API 576, API 527, BS EN ISO 4126, and API 598 across Sharjah, Dubai, Abu Dhabi, and the wider UAE. Explore the PRV testing services page for the full scope of valve sizes and testing capability.
For facilities running broader pressure instrumentation alongside PRVs, our pressure calibration services cover the gauges, transmitters, and dead weight testers used throughout the same process systems these relief valves protect.
Frequently Asked Questions
What is the difference between pop testing and seat tightness testing? Pop testing confirms the valve opens at its correct set pressure. Seat tightness testing confirms the valve doesn't leak while closed under normal operating pressure. A valve needs to pass both to be considered fully functional and properly certified.
What test medium is used for PRV seat tightness testing? API 527 specifies air or nitrogen for valves in compressible fluid service, and water for valves in non-compressible fluid service, with the appropriate choice depending on the valve's actual process application.
Why do metal-seated and soft-seated valves have different leakage criteria? Metal-seated valves are generally held to a maximum allowable leakage rate, since achieving zero leakage with metal-to-metal contact is impractical, while soft-seated valves, using elastomeric or polymer seating materials, are typically expected to show no leakage at all during the test period.
How is the correct PRV testing interval determined? Testing frequency depends on the valve's service medium, operating history, applicable regulatory or insurance requirements, and manufacturer recommendations, with intervals often refined over time based on actual observed performance at a specific installation rather than a single fixed schedule.
What happens if a valve fails testing? Depending on the failure mode, the valve may require seat lapping to restore proper sealing contact, spring replacement, or in more severe cases full valve replacement, followed by retesting and recertification before it's returned to service.
Closing Thoughts
PRV testing UAE refineries, petrochemical plants, and process facilities depend on protects against the specific kind of failure that has no early warning: a safety device that hasn't been called upon in years suddenly needing to perform exactly when the system is already in trouble. Documented pop and seat tightness testing, performed to API 576, API 527, and BS EN ISO 4126, is what keeps that protection genuinely trustworthy rather than assumed.
To schedule PRV testing or broader pressure system verification across the UAE, reach out through the General Tech Services contact page, or explore the full range of ISO 17025 accredited calibration and testing services available across every Emirate.